
Co Down-based slurry specialist SlurryQuip will display a selection of its latest products at the FTMTA Show, including its remote engine pump, HiLift umbilical dribble bar and the Borger RC150 mobile slurry separator.
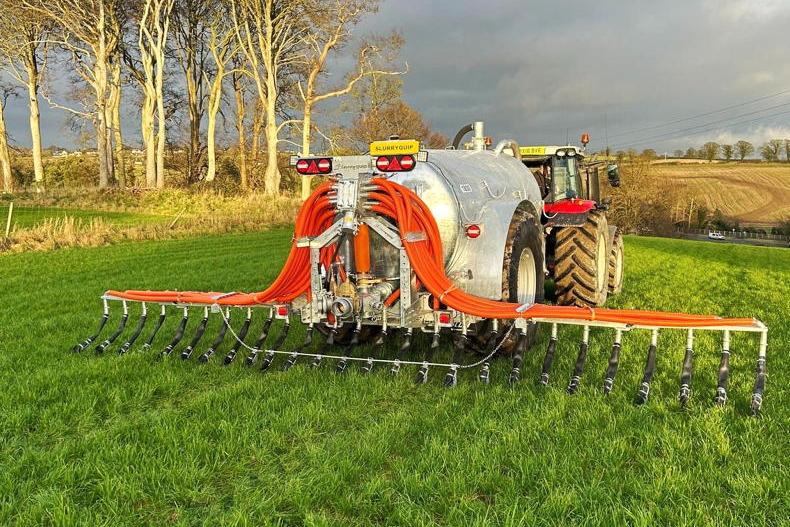
SlurryQuip has said its main products at this year’s FTMTA Show will be the SlurryQuip Engine Pump, alongside its 12m HiLift umbilical dribble bar and the SlurryQuip Borger RC150 mobile slurry separator.
SlurryQuip’s engine pump is powered by a Stage V-compliant CAT 188hp engine, while the unit is controlled through SlurryQuip’s Infinity remote control system, with radio, GSM and satellite connectivity.
The manufacturer says the system has undergone field testing across Ireland, successfully operating through both GSM and satellite connections in a range of locations and conditions.
Designed to improve efficiency, reduce labour requirements and keep hours off the tractor, the system provides live monitoring of pressure, flow, fuel consumption, volume pumped and engine performance.
The unit is available with either a Veneroni or Bauer pump, in skid-mounted or trailer-mounted configurations.
12m HiLift umbilical dribble bar
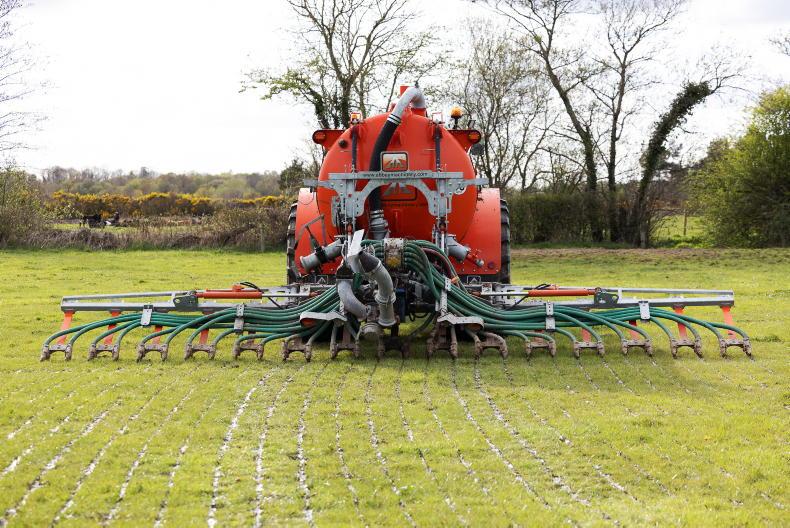
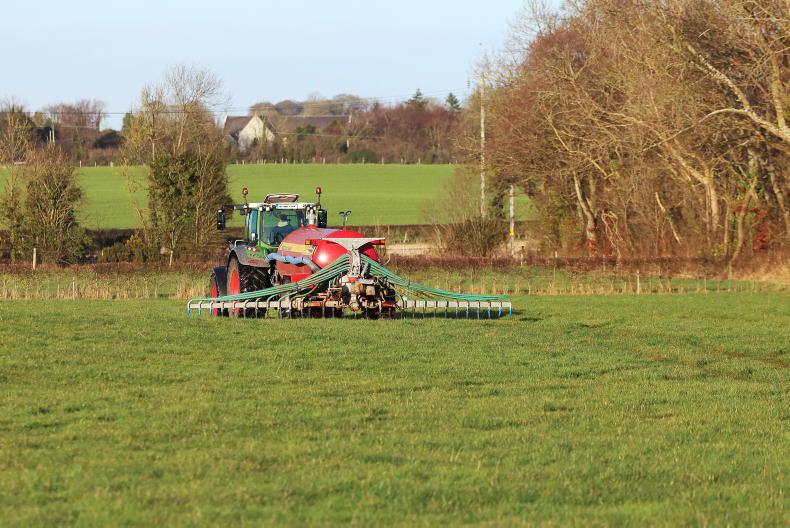
Also on display will be the firm’s 12m double-macerator umbilical dribble bar with the HiLift reel system.
Its hydraulic lifting mechanism raises the reel above the swinging arm, allowing spreading with the bobbin still fitted.
SlurryQuip notes this is particularly useful when moving between several small fields on the same farm.
The reel can also be dropped, interchanged with the front reeler or removed to reduce weight. Each reel can carry up to 1,200m of hose. The HiLift system is available on both its 12m and 15m models.
RC150 mobile slurry separator
Completing the display will be the RC150 mobile slurry separator. This RC 150 offers self-acclaimed 100m3/hr to 120m3/hr throughput capacity in typical dairy slurry.
This solution is mounted on to a purpose-built galvanised trailer unit, with an on-board generator up front. All its functions be can fully radio controlled, while an on-board, load-sensing slurry pump provides flow to and from the separator.